Geltungsbereich
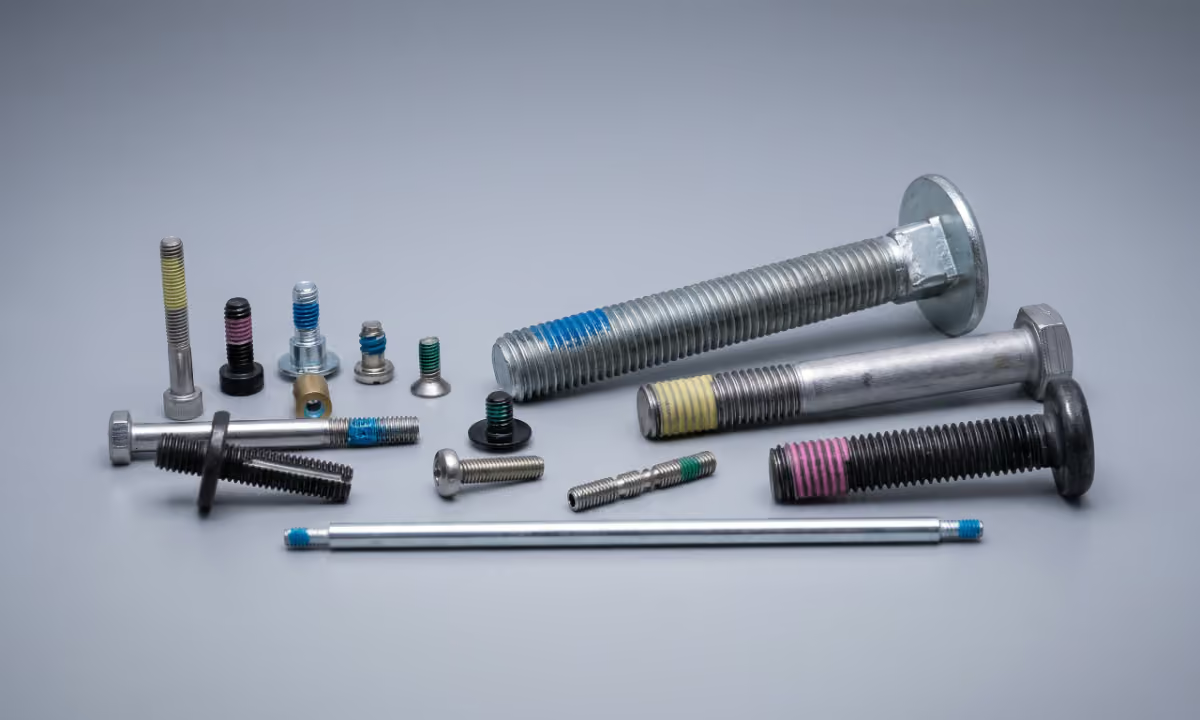
Von genormten Gewindesicherungen bis zu extremen Speziallösungen. Die DIN 267 Teil 27 und Teil 28 beschreiben die Anforderungen an klebende und klemmende Gewinde-Sicherungen. Doch moderne Verbindungstechnik geht weit darüber hinaus.
Neben mikroverkapselten Klebstoffbeschichtungen und klemmenden Sicherungssystemen bieten wir auch spezialisierte mechanische Gewindesicherungen für anspruchsvolle Anwendungen. Welche Lösung die richtige ist, hängt von Temperatur, Vibration, Gewindeabmessung, Werkstoff und den geforderten Sicherungs-Eeigenschaften ab.
−60 bis +1.000 °C
TEMPERATURBEREICH
Bis M39
Gewinde
DIN + Spezial
SICHERUNGSTECHNOLOGIEN
Nahezu unbegrenzt
Lagerbeständigkeit
Four ways to lock a thread.
Prevailing torque or adhesive, with plastic or with filament: the four processes differ in thread range, temperature range and reusability. We check from your drawing which one fits your component.
Tuflok
Nylon layer, clamps and seals
The Tuflok coating is an elastic, abrasion-resistant nylon layer on a section of the thread. It locks against vibration and loosening, seals against liquids and gases when applied all round, and remains reusable.
Suitable from M1
Minus 56 to 120 °C, Nytemp up to 200 °C
Reusable
Protects surfaces and mating parts
Filament locking (NormTight)
Carbon filament in the thread instead of adhesive
With NormTight, a groove is made in the thread and an elastically deformed special filament is pressed in. The connection withstands vibration, needs no adhesive and keeps the tightening torque constant over many assemblies. On request, we are also happy to offer the special solution in copper, aluminium, titanium, steel or stainless steel.
Exceeds DIN 267 Part 28
Recyclable, without adhesive
No particle shedding
Filament also available colourless
Prevailing torque thread locking
Prevailing torque to DIN 267 Part 28
A plastic coating clamps the connection and prevents it from coming completely loose on its own. Applied as a patch or all round, distinguishable in several colours. According to the standard, the coating is intended for one assembly.
M3 to M16
Minus 50 °C to 120 °C
As a patch or all round
2 application types
Shelf life of up to four years in accordance with DIN 267-27 and DIN 267-28, depending on coating, intended use and storage conditions. Individual details are available on request.
Micro-encapsulation DIN 267
Adhesive to DIN 267 Part 27
With micro-encapsulated screws, the adhesive sits in capsules on the thread. On tightening they burst, the adhesive spreads and cures in the thread. According to the standard, applied all round and intended for one assembly.
Always as an all-round coating
Shelf life of up to four years in accordance with DIN 267-27 and DIN 267-28, depending on coating, intended use and storage conditions. Individual details are available on request.
Position of the coating
Not the whole thread is coated.
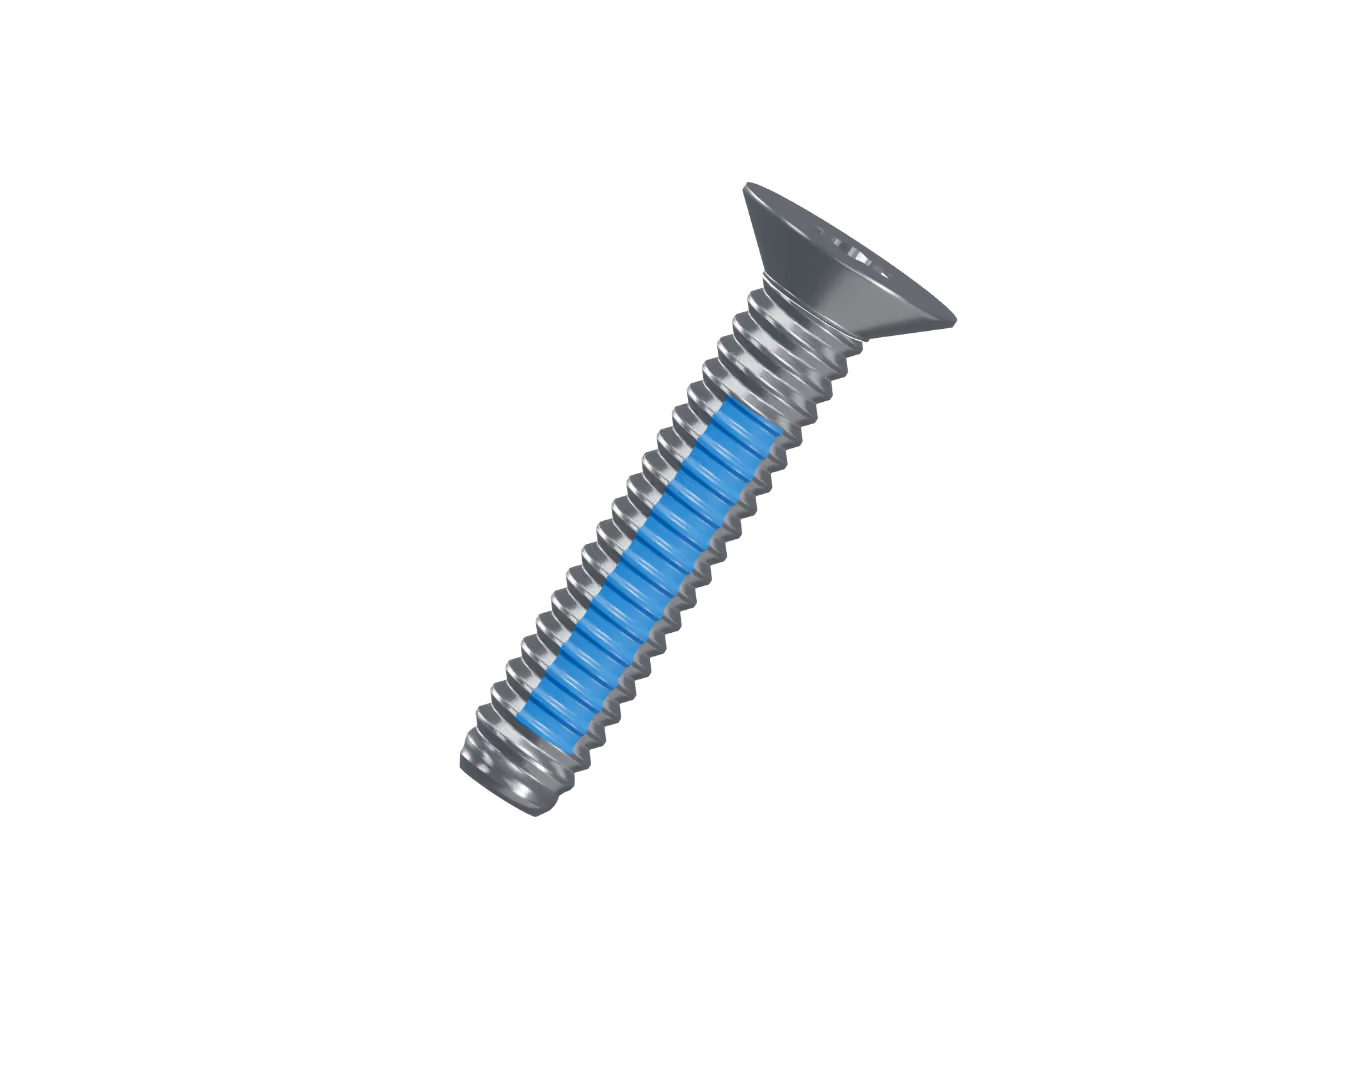
The first two to three turns remain free, so that the screw starts cleanly and does not jam when screwed in. Only after that does the coating cover four to six turns, as a patch or all round. Anyone looking for a strip coating usually means one of these two versions.
If the connection also has to seal, the coating runs over 360 degrees. We agree a different position or length with you in advance.
With every delivery you receive the documents that your approval requires. What is inspected for this and what the certificate states can be found on the quality page.
01
Screwing in
The first 2 to 3 turns remain free
02
Locking
4 to 6 turns carry the coating
03
Sealing
360 degrees all round when sealing is needed
Three designs on the thread.
01
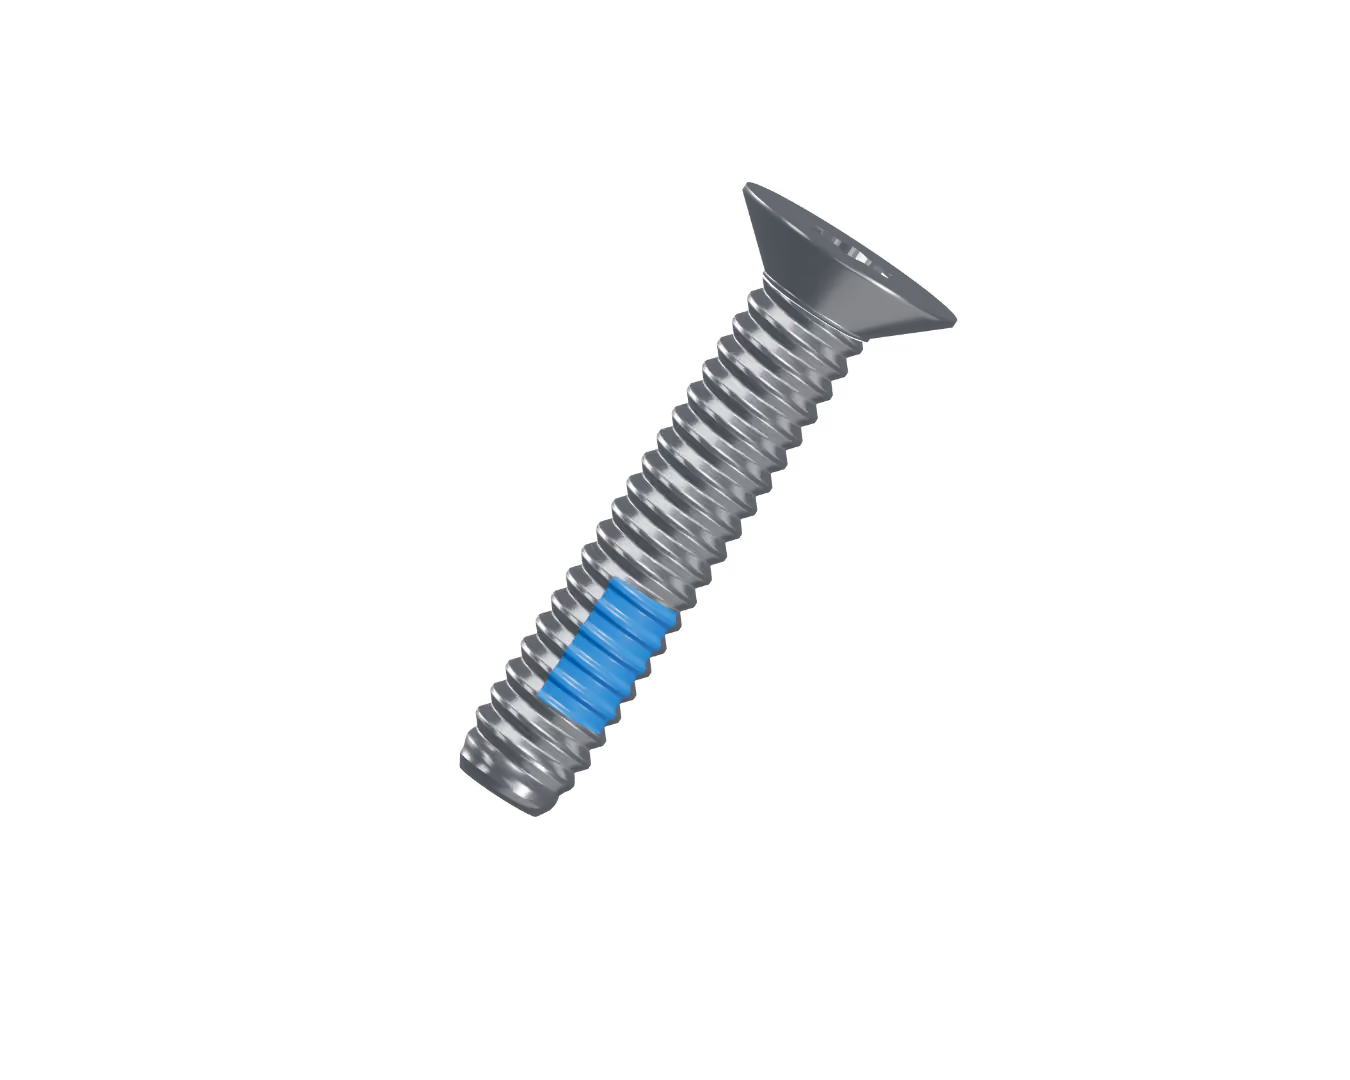
Patch coating
A patch over a few turns. The most common version: it locks the connection without closing it for good.
02
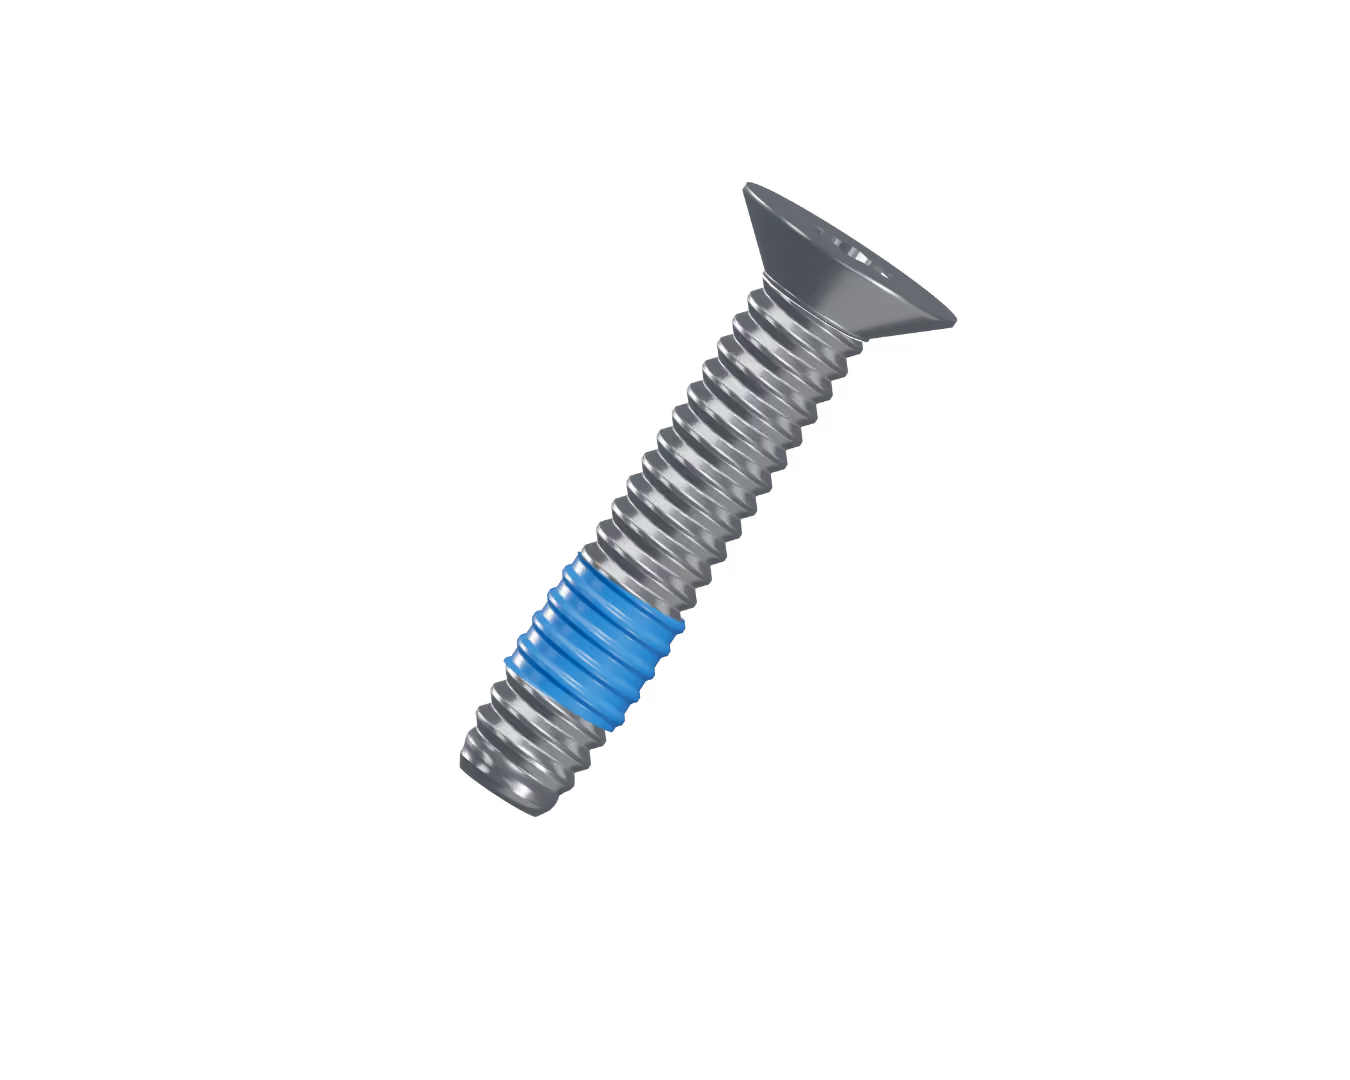
All-round coating
Over 360 degrees around the thread. Locking and sealing in one operation, when nothing is to get through.
03
Filament locking
A filament, inserted into a groove in the thread. The third version alongside patch and all-round, more on this under NormTight.
Process questions
Give us the three answers by phone or with your inquiry, and we will propose the process.
Should the screw come undone again?
Then prevailing torque to DIN 267 Part 28 or with Tuflok. The plastic holds and releases again when loosened. The filament solution is also reusable several times
Should the connection be sealed?
Then all round over 360 degrees. Locking and sealing run in one operation, a second step is not needed. Alternatively, ND Plastisol JX-185 seals and dampens.
How hot does it get at the screw?
Part 28 applies up to 120 degrees, Part 27 up to 100 degrees. Above that, there are dedicated coatings such as Tuflok Nytemp.
Measurement is to DIN 267 with a test nut made exactly for this purpose: 0.8 to 0.9 d high, countersunk 120 degrees on both sides and at least as strong as the screw. The thread is bright or black from heat treatment and free of oil, grease, chips and burrs. Only under these conditions can the prevailing torque and breakaway torque of two coatings be compared. How often a locked screw can be loosened and retightened depends on the process.
Clamping or bonding
Should the connection come undone later, or never again? Standard and design depend on that.
Prevailing torque coating
Standard
DIN 267 Part 28
Effect
A plastic clamps the connection in the thread. As a loss prevention device, it prevents screws from coming completely loose.
Designs
As a patch or all round, also in different colours for identification.
What you need to watch out for
According to the standard, intended for one assembly, as an adjusting or setting screw also several times. If the connection is loosened more often, Tuflok or NormTight is a better fit.
Adhesive coating, micro-encapsulated
Standard
DIN 267 Part 27
Effect
On tightening, microcapsules burst, the adhesive spreads, cures in the thread and locks against loosening.
Designs
Always all round. Products such as Precote differ in curing time and breakaway torque.
What you need to watch out for
Store dry, moisture is the only real enemy. If the coating changes colour, that is not a defect as long as the test values are met.
Note
The information on this page comes from the standards and from manufacturer data and is intended for guidance. Check the process under your operating conditions before series use, ideally with a trial coating on your component. We accept no liability for the data or for results.
Questions
What design engineering and purchasing ask.
01
What is thread locking to DIN 267?
DIN 267 is the series of standards for technical delivery conditions of fasteners. DIN 267-27 covers micro-encapsulated screw locking, that is steel screws with an adhesive coating, and DIN 267-28 steel screws with a prevailing torque coating. Part 27 covers coarse threads M3 to M39 and minus 50 to plus 100 °C. Part 28 goes up to plus 120 °C, depending on the application specification up to 150 or 200 °C, for coarse threads up to M18 in the 2026-02 edition, previously up to M16.
02
What is the difference between prevailing torque and adhesive thread locking?
A prevailing torque coating to DIN 267 Part 28 holds the screw through friction. It prevents the connection from coming completely loose, but not from loosening, and according to the standard is intended for single use, as an adjusting or setting screw also several times. An adhesive coating to Part 27 cures in the thread after tightening and counteracts loosening. It is always an all-round coating and is also intended for single use.
03
What is Tuflok and how often can it be used?
Tuflok is a highly elastic, abrasion-resistant nylon layer made of polyamide 11. It is applied to a section of the thread after induction heating, does not dry out and does not shrink. Tuflok screws are reusable, five assemblies are intended. The temperature range is minus 56 to 120 °C, with Nytemp up to 200 °C. As an all-round coating, Tuflok seals against liquids and gases, suitable from M1.
04
How is the breakaway torque tested?
To DIN 267 with a test nut that is 0.8 to 0.9 d high, countersunk 120 degrees on both sides and at least as strong as the screw, with thread tolerance 6H. The thread is bright or black from heat treatment and free of oil, grease, chips and burrs. Other test nuts are only permitted by agreement. We agree different torques or test methods with you in advance, usually together with a trial coating on your component.
05
What is filament locking, and when is it the better choice?
With the NormTight filament locking, a groove is milled into the thread to just below the minor diameter and an elastically deformed special filament is pressed in. The filament needs no adhesive, sheds no particles and is also available colourless. The breakaway torque exceeds the requirement of DIN 267 Part 28, and the connection can be screwed together several times. It fits where particles, chemicals or single use are a problem, for example in medical technology or electronics.
06
Do I have to apply the thread locking myself?
No. You order the fastener with the thread locking already applied, that is a screw, threaded bolt or special part made to drawing, and assemble as usual. Screws with locking varnish or a factory-applied coating save you additional mechanical locking elements and a step in assembly. The first 2 to 3 thread turns remain free, and the coating covers the following 4 to 6. We agree any requirements for position and length with you in advance.